A chemical reactor agitator that cannot manage competing demands-exothermic heat generation, precise feed rates, viscosity changes across reaction stages-fails to deliver the uniformity that chemistry demands. Uncontrolled hotspots cause side reactions, imprecise blending creates off-spec batches, and inadequate wall contact prevents heat removal during critical phases. Premix Technologies, based in Ahmedabad, Gujarat, has engineered the Chemical Reactor Agitator to solve exactly this challenge across pharmaceutical synthesis, fine chemical manufacturing, and specialty polymer production, where reaction kinetics and thermal management decide product purity and yield.
Every Chemical Reactor Agitator maintains homogeneous mixing conditions throughout the entire reaction cycle, handles viscosity evolution as monomers polymerize or solutions concentrate, and manages heat transfer with the precision that chemical processes require without forcing the reaction away from its optimal conditions. A properly designed Chemical Reactor Agitator keeps reaction rates consistent, prevents dead zones where side reactions propagate, and plants that need equipment engineered for actual feed rates, reaction exotherms, and final product chemistry usually find their way to Premix Technologies.
| Aspect | Typical Capability / Range | Value Proposition for Reactor Applications |
|---|---|---|
| Motor Drive Power | From 2.2 kW to over 1000 kW | Provides the precise power required for intense mixing, high-viscosity processing, and effective mass/heat transfer in reactors of all scales and chemistries. |
| Reactor Volume Adaptation | Suitable for reactors from 1 m³ to over 500 m³ | Designed for optimal mixing performance across a wide range of reactor sizes, ensuring consistent conditions and efficient reactions from pilot to full production scale. |
| Operating Pressure | From Atmospheric to over 300 Bar (30 MPa) | Engineered for high-pressure reactor applications, ensuring mechanical integrity and reliable sealing under extreme conditions common in chemical synthesis. |
| Operating Temperature | From -50°C to over +400°C | Capable of operating in a broad spectrum of temperatures, facilitating precise thermal control for exothermic or endothermic reactions. |
| Product Viscosity Handling | From 1 cP (water-like) up to 1,000,000+ cP (for polymers/pastes) | Versatile mixing capabilities to effectively agitate fluids across an immense viscosity range, crucial for diverse chemical reactions and product states. |
| Impeller Diameter | From 200 mm to over 4000 mm | Custom-sized impellers optimized for specific reactor geometries and reaction needs, ensuring efficient fluid dynamics for mass transfer, solids suspension, and heat exchange. |
| Shaft & Bearing System | Heavy-duty, high-precision shafts (e.g., 50 mm to 500 mm diameter), engineered bearing supports | Designed for exceptional rigidity and minimal deflection under high loads, critical for maintaining seal integrity and smooth operation in demanding reactor environments. |
| Impeller Technology | Axial Flow (Hydrofoils, Pitched Blades), Radial Flow (Rushton, Disc), High Shear, Anchor, Helical Ribbon, Gassing Impellers, Special Custom Designs | A comprehensive array of impeller types selected to precisely match reaction kinetics, phase dispersion, and desired mixing intensity for optimal process outcomes. |
| Material Construction (Wetted) | SS304, SS316L, Duplex Stainless Steels, Hastelloy, Inconel, Titanium, Glass-Lined Steel, PTFE/Rubber Linings | Materials are rigorously chosen for superior resistance to the specific corrosive and erosive nature of reaction media, ensuring product purity and equipment longevity. |
| Seal System | Robust Mechanical Seals (single, double, cartridge), Magnetic Drives, Packed Gland Seals | Advanced sealing solutions engineered for high-pressure, high-temperature, corrosive, or sterile environments, ensuring zero leakage and maximum safety. |
| Compliance & Safety | Designed to ASME, PED, ATEX/IECEx (Ex-proof), cGMP (for Pharma), and other relevant industry standards | Strict adherence to international safety and quality regulations, providing assurance for operators and facilitating regulatory approvals. |
Most vendors supply a one-size-fits-all reactor agitator from inventory. Very few investigate the actual reaction sequence, understand where heat generation peaks, or verify that the agitator can handle the viscosity jump when a solution goes from dilute to near-solid during synthesis. Premix Technologies spends engineering time exactly there, understanding the chemistry first, then sizing the agitator around it. That discipline is why the company ranks among the dependable Chemical Reactor Agitator Manufacturers and Chemical Reactor Agitator Suppliers that chemical plants return to for both single-step reactions and multi-stage processes. Export demand has followed the same track record, and Premix Technologies now stands among trusted Chemical Reactor Agitator Exporters serving international pharmaceutical and fine chemical customers seeking reliable synthesis performance.
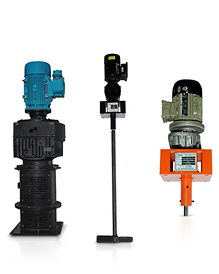
Homogeneous Mixing Throughout Reaction Cycles
A chemical reactor agitator from Premix Technologies circulates the entire batch volume continuously, ensuring fresh reactant surfaces meet catalyst or reagent additions uniformly. No concentration gradients, no local hotspots where side reactions accelerate-every molecule in the reactor follows the same exposure to reaction conditions, keeping selectivity high and by-product formation low.
Precise Heat Transfer Management
Exothermic reactions generate dangerous temperature rises if mixing is passive or inadequate. Premix Technologies sizes the Chemical Reactor Agitator and impeller geometry to pull heated medium from the reaction zone toward cooled vessel walls, shedding heat efficiently without requiring oversized jacket systems. Temperature control becomes predictable, and runaway risk drops when mixing quality is engineered into the design from the start.
Viscosity Evolution Handling
Reactions that build polymer chains or concentrate solutions shift viscosity dramatically mid-process. Light stirring that works at batch start becomes useless when the medium turns thick. Premix Technologies specifies impeller type and drive power for every Chemical Reactor Agitator based on the full viscosity range the reaction will see, so agitation remains effective from monomer feed through gel-point curing without motor strain or seal failure.
Robust Mechanical Stability
Continuous high-speed operation under exothermic load and changing viscosity demands more than a standard stirrer. Premix Technologies builds every Chemical Reactor Agitator with reinforced shafts, precision-aligned bearing supports, and sealed drive couplings to handle sustained mixing duty without vibration creep or premature seal wear, keeping the reactor running through multi-hour synthesis cycles without maintenance interruption.
Corrosion & Solvent Resistance
Chemical reactors handle aggressive organic solvents, caustic or acidic media, and specialty reagents that erode standard materials quickly. Premix Technologies manufactures wetted components of every Chemical Reactor Agitator in SS316L, Hastelloy, or Teflon-lined options matched to the specific solvent system and reaction chemistry, ensuring agitator life matches the reactor vessel life.
Explosion-Proof & Hazardous Compliance
Where Chemical Reactor Agitators operate in solvent-rich environments or near flammable vapor zones, Premix Technologies supplies ATEX and IECEx certified motor configurations with intrinsically safe wiring and containment enclosures, so the agitator never becomes the ignition source in an otherwise controlled chemical facility.
Multi-Purpose Reaction Support
Acid-base neutralizations, polymerizations, condensations, additions, and curing reactions-a single Chemical Reactor Agitator engineered for the specific process handles most synthesis work without equipment swaps or reactor redesign. That flexibility is why Premix Technologies units appear across pharmaceutical pilot plants, specialty chemical labs, and production facilities alike.
Custom Impeller & Shaft Configuration
Anchor impellers, turbines, helical ribbons, and combination geometries behave differently as reaction viscosity and heat load change. Premix Technologies selects impeller type and shaft length for each Chemical Reactor Agitator based on the actual reaction chemistry and thermal profile, ensuring optimal mixing at every stage from feed addition through final curing.
Heavy-Duty Drive & Mechanical Design
A reinforced drive system, precision-engineered mounting, and properly rated motor combine to separate a Chemical Reactor Agitator built to deliver batch after batch from one suffering premature seal or bearing failure. Field experience shows Premix Technologies units hold performance across hundreds of reaction cycles without degradation.
Minimized Batch Loss to Mechanical Failure
Every synthesis run that completes without agitator downtime is a batch that meets specification and hits market on schedule. That’s the reliability focus Premix Technologies engineers into every Chemical Reactor Agitator design.
Custom Engineering:
Each reactor agitator is typically a custom-engineered solution, designed in close consultation with the client to precisely match the reactor geometry, process chemistry, and performance targets.
Range of Scales:
From pilot-scale reactors for R&D to very large production-scale chemical synthesis vessels.
Premix Technologies has built a reputation among reliable Chemical Reactor Agitator Manufacturers, Chemical Reactor Agitator Suppliers, and Chemical Reactor Agitator Exporters across pharmaceutical and specialty chemical synthesis, including:
Pharmaceutical Active Ingredient Synthesis – maintaining homogeneous conditions during multi-step synthesis and intermediate reactions Fine Chemical & Specialty Synthesis – precise mixing during acid-base neutralizations and reagent additions Polymer & Resin Polymerization – managing exothermic heat and viscosity evolution during monomer coupling and curing Catalyst Preparation & Activation – controlled mixing during catalyst synthesis and dispersion into reaction media Emulsion & Suspension Formulation – gentle yet thorough mixing to maintain product uniformity without excessive shear Condensation & Coupling Reactions – uniform reactant distribution and byproduct removal during multi-stage synthesis Custom Organic Synthesis – flexible agitation for small-batch and intermediate-scale chemical development
Delivering precision-engineered mixing and dosing solutions across diverse industrial sectors with reliability and performance.
Before any Chemical Reactor Agitator goes into production, the Premix Technologies engineering team runs Computational Fluid Dynamics studies to predict how the impeller will circulate reactants, manage heat dissipation, and maintain mixing intensity across the viscosity range the actual reaction will see. It checks flow patterns, identifies dead zones, predicts hotspot locations, and validates power requirements at peak viscosity, solving design problems in simulation before they become expensive failures in the lab or plant.
Chemical reactor agitation sounds routine until it has to hold homogeneity through an exothermic peak, handle a tenfold viscosity jump mid-synthesis, and prevent side reactions that ruin batch chemistry-that’s the engineering detail Premix Technologies never overlooks on any Chemical Reactor Agitator it delivers. The process starts with a conversation about reaction chemistry and thermal profile, then moves through design verification, manufacturing precision, and reactor commissioning support. Based in Ahmedabad, the team has built the track record that chemical manufacturers seeking reliable Chemical Reactor Agitator Suppliers and Chemical Reactor Agitator Exporters have learned to trust.
Reach out to Premix Technologies for equipment designed around the actual reaction kinetics and heat load, not a generic catalog unit forced to work. Domestic and international pharmaceutical and chemical buyers work with Premix Technologies as their preferred Chemical Reactor Agitator partner.
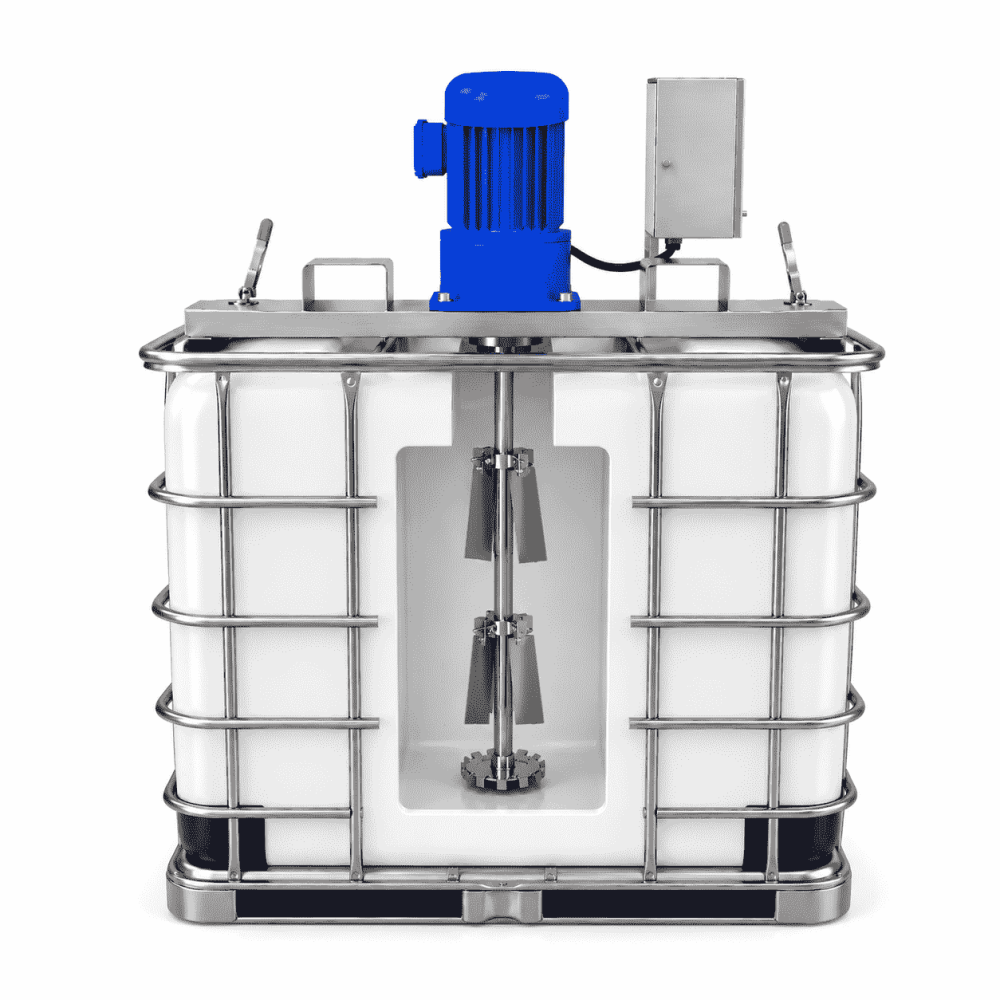
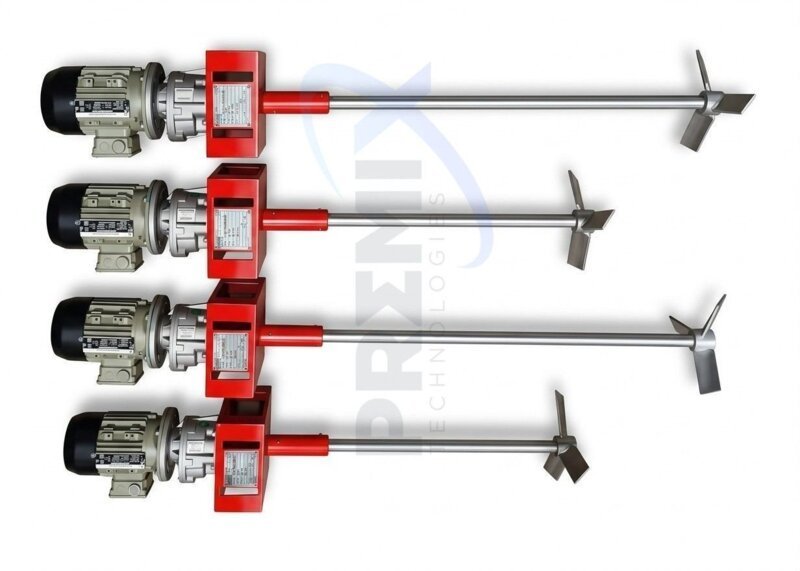
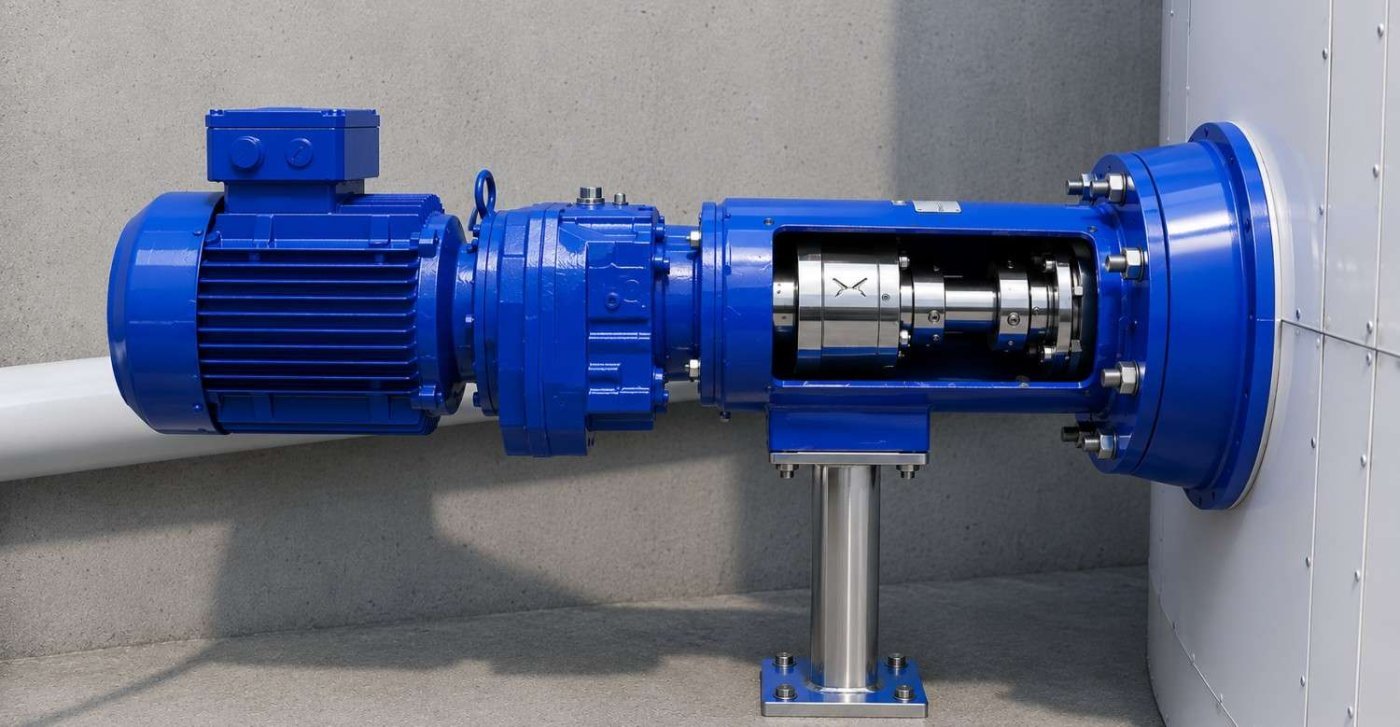
It maintains homogeneous mixing throughout chemical synthesis and polymerization reactions, manages exothermic heat generation, handles viscosity changes as reactions progress, and prevents dead zones where side reactions could develop. Premix Technologies builds Chemical Reactor Agitators for pharmaceutical intermediate synthesis, fine chemical manufacturing, polymer polymerization, and any reaction requiring precise thermal and mixing control to achieve high yield and product purity.
Pharmaceutical Active Ingredient (API) manufacturing, fine chemical synthesis, specialty polymer and resin production, catalyst preparation, organic synthesis development, custom chemical manufacturing, and industrial chemical processing-the Ahmedabad facility has supported synthesis requirements across most of these sectors.
Premix Technologies reviews the actual reaction chemistry, feeds rates, exothermic profile, and viscosity range from start to finish. From there, impeller type, shaft length, drive motor power, and thermal management design all get customized around the specific reaction requirements before manufacturing begins.
Yes, reputable Chemical Reactor Agitator Suppliers engineer the drive power and impeller geometry for the peak viscosity condition, ensuring agitation remains effective throughout the entire reaction cycle. Premix Technologies sizes every agitator to handle the full viscosity range without motor overload or mixing failure at any reaction stage.
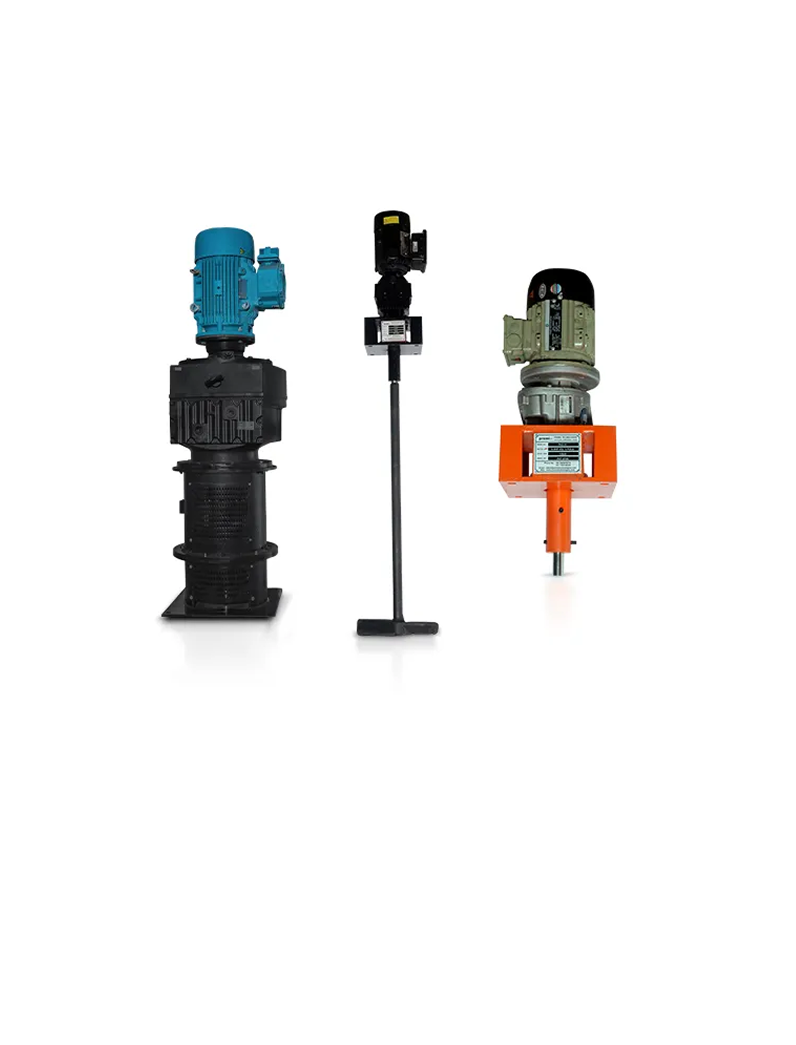
Yes. Shaft, motor, gearbox or direct drive, impeller, bearing supports, seals, and mounting brackets come pre-assembled and tested together. Optional temperature sensors, viscosity monitoring, and agitation speed control interfaces can be integrated for process optimization and batch documentation compliance.
Have questions about our products or need a customized solution? Our team is ready to assist you with expert guidance, technical support, and reliable service. Reach out to us today and let’s build efficient solutions together.