A biogas digester that isn’t mixed properly never produces the gas yield the process design intended. Sludge settles into a crust at the top, solids sink and compact at the base, and the microbial population ends up starved in one zone while flooded in another. Premix Technologies, based in Ahmedabad, Gujarat, has been engineering the Central Mixer for Biogas Digesters to solve exactly this problem across municipal biogas plants, agricultural digesters, and industrial anaerobic digestion systems that depend on consistent solids suspension and homogeneous digestion.
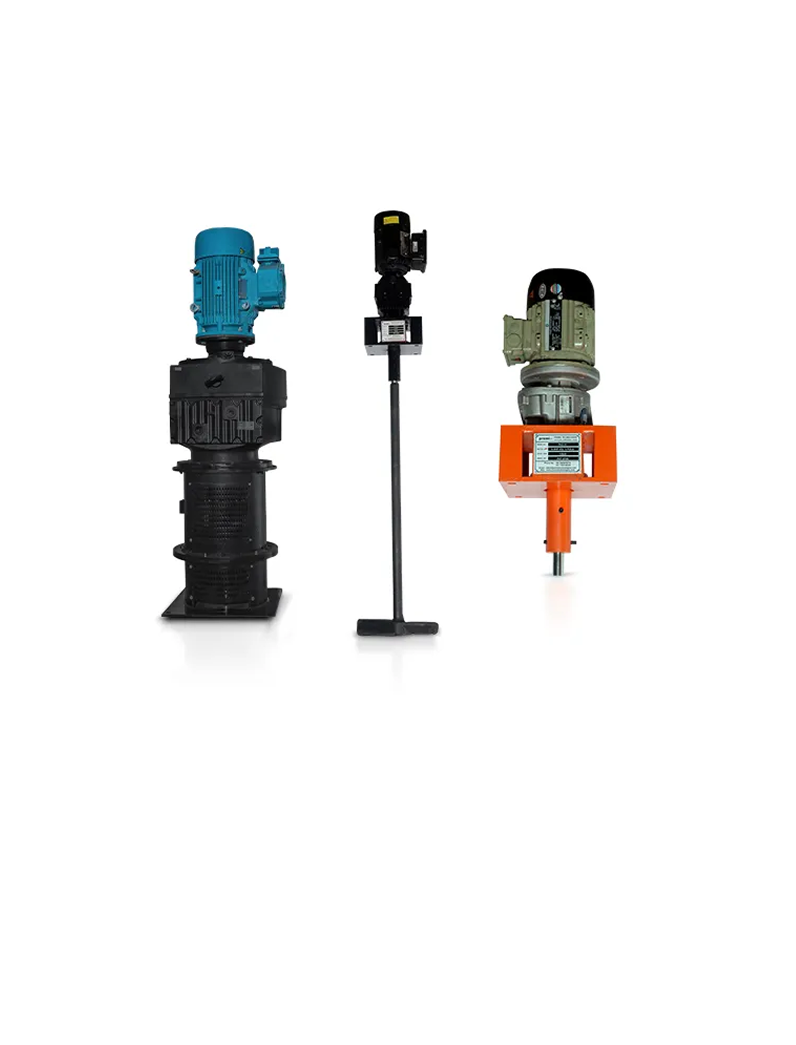
Every Central Mixer for Biogas Digesters drives a centrally mounted impeller through the digester slurry, breaking up scum layers, preventing sedimentation, and keeping the biological process stable without disturbing the anaerobic balance of the tank. A properly built Central Mixer for Biogas Digesters keeps circulation consistent across the entire digestion cycle, and plants that need a unit sized around actual tank volume and feedstock type, not a catalog part forced to fit, usually end up working with Premix Technologies.
| Aspect | Typical Capability / Range | Value Proposition for Reactor Applications |
|---|---|---|
| Motor Drive Power | From 2.2 kW to over 1000 kW | Provides the precise power required for intense mixing, high-viscosity processing, and effective mass/heat transfer in reactors of all scales and chemistries. |
| Reactor Volume Adaptation | Suitable for reactors from 1 m³ to over 500 m³ | Designed for optimal mixing performance across a wide range of reactor sizes, ensuring consistent conditions and efficient reactions from pilot to full production scale. |
| Operating Pressure | From Atmospheric to over 300 Bar (30 MPa) | Engineered for high-pressure reactor applications, ensuring mechanical integrity and reliable sealing under extreme conditions common in chemical synthesis. |
| Operating Temperature | From -50°C to over +400°C | Capable of operating in a broad spectrum of temperatures, facilitating precise thermal control for exothermic or endothermic reactions. |
| Product Viscosity Handling | From 1 cP (water-like) up to 1,000,000+ cP (for polymers/pastes) | Versatile mixing capabilities to effectively agitate fluids across an immense viscosity range, crucial for diverse chemical reactions and product states. |
| Impeller Diameter | From 200 mm to over 4000 mm | Custom-sized impellers optimized for specific reactor geometries and reaction needs, ensuring efficient fluid dynamics for mass transfer, solids suspension, and heat exchange. |
| Shaft & Bearing System | Heavy-duty, high-precision shafts (e.g., 50 mm to 500 mm diameter), engineered bearing supports | Designed for exceptional rigidity and minimal deflection under high loads, critical for maintaining seal integrity and smooth operation in demanding reactor environments. |
| Impeller Technology | Axial Flow (Hydrofoils, Pitched Blades), Radial Flow (Rushton, Disc), High Shear, Anchor, Helical Ribbon, Gassing Impellers, Special Custom Designs | A comprehensive array of impeller types selected to precisely match reaction kinetics, phase dispersion, and desired mixing intensity for optimal process outcomes. |
| Material Construction (Wetted) | SS304, SS316L, Duplex Stainless Steels, Hastelloy, Inconel, Titanium, Glass-Lined Steel, PTFE/Rubber Linings | Materials are rigorously chosen for superior resistance to the specific corrosive and erosive nature of reaction media, ensuring product purity and equipment longevity. |
| Seal System | Robust Mechanical Seals (single, double, cartridge), Magnetic Drives, Packed Gland Seals | Advanced sealing solutions engineered for high-pressure, high-temperature, corrosive, or sterile environments, ensuring zero leakage and maximum safety. |
| Compliance & Safety | Designed to ASME, PED, ATEX/IECEx (Ex-proof), cGMP (for Pharma), and other relevant industry standards | Strict adherence to international safety and quality regulations, providing assurance for operators and facilitating regulatory approvals. |
Plenty of vendors will sell a Central Mixer for Biogas Digesters straight off a standard list. Very few work out what a specific tank geometry, feedstock consistency, or gas production target actually needs before quoting a price. Premix Technologies spends most of its engineering time exactly there, and that discipline is why the company is counted among the dependable Central Mixer for Biogas Digesters Manufacturers and Central Mixer for Biogas Digesters Suppliers that biogas plant operators keep coming back to. Export orders have followed the same pattern, and Premix Technologies now ranks among the trusted Central Mixer for Biogas Digesters Exporters serving customers well beyond India.
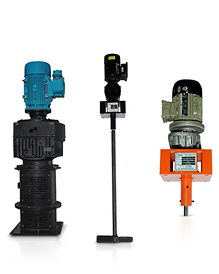
Flow & Turnover
An impeller mounted off-centre or undersized only disturbs part of a digester tank. Premix Technologies sizes each Central Mixer for Biogas Digesters to pull the full slurry volume into circulation, so feedstock, bacteria, and biogas bubbles stay evenly distributed instead of stratifying toward the base or crusting at the surface.
Process Uniformity
Uneven mixing causes more trouble downstream than most operators expect. Scum formation, foaming, and inconsistent retention time all trace back to weak agitation. Steady circulation from a well-sized Central Mixer for Biogas Digesters keeps digestion conditions consistent through every feed cycle.
Rapid Dispersion
Left under-mixed, fresh feedstock stays concentrated near the inlet instead of reaching the full microbial population. The impeller on a Premix Technologies Central Mixer for Biogas Digesters works against that, achieving uniform dispersion without generating excess turbulence that could disrupt methanogenic activity.
Robust Mechanical Design
Running continuously for years is where lighter units show wear – shaft flexing, seal leakage, off-centre wobble. Premix Technologies sizes the shaft, bearing support, and drive on every Central Mixer for Biogas Digesters to avoid that, keeping vibration and misalignment out of the picture over years of continuous plant operation.
Corrosion & Wear Resistance
Some digesters handle mild agricultural slurry. Others handle high-solids municipal sludge or corrosive H2S-laden environments. Premix Technologies builds the wetted parts of every Central Mixer for Biogas Digesters in SS304, SS316L, or other resistant alloys, chosen according to the actual feedstock chemistry involved.
Hazardous Area Compliance
Where a Central Mixer for Biogas Digesters operates inside or near a gas-tight digester dome, Premix Technologies supplies drives in explosion-proof configurations, built to ATEX and IECEx standards, so the mixer never becomes the weak link in an otherwise controlled biogas process.
Multi-Purpose Agitation
Feedstock blending, scum breaking, solids suspension, and general tank circulation – a single Central Mixer for Biogas Digesters handles most of it without a different machine for each stage. That range is why Premix Technologies units turn up across municipal biogas plants, agricultural digesters, and industrial anaerobic digestion lines alike.
Custom Impeller Selection
Hyperboloid, propeller, and pitched-blade impellers behave differently once tank shape and solids loading change. Premix Technologies picks the impeller for each Central Mixer for Biogas Digesters based on what the actual digestion process demands.
Heavy-Duty Construction
A reinforced central shaft, a properly rated motor, and a mounting structure that doesn’t work loose under continuous digester duty – that combination separates a Central Mixer for Biogas Digesters built to last from one that needs attention within months.
Minimized Downtime
Every hour a biogas plant doesn’t spend draining a digester to service the mixer is an hour gas production keeps running without interruption. That’s the target Premix Technologies engineers toward with every Central Mixer for Biogas Digesters built.
Custom Engineering
There’s no catalog page at the start of the process. Engineering begins with tank dimensions, feedstock type, and the actual mixing target, and the Central Mixer for Biogas Digesters gets designed from there.
Range of Scales
Whether it’s a small farm-scale digester or a full municipal biogas plant, the engineering discipline behind a Central Mixer for Biogas Digesters doesn’t change just because the scale does.
Premix Technologies has built a reputation among reliable Central Mixer for Biogas Digesters Manufacturers, Central Mixer for Biogas Digesters Suppliers, and Central Mixer for Biogas Digesters Exporters across a wide spread of industries, including:
Delivering precision-engineered mixing and dosing solutions across diverse industrial sectors with reliability and performance.
Before any Central Mixer for Biogas Digesters gets built, the Premix Technologies engineering team runs Computational Fluid Dynamics studies to see how the impeller will circulate slurry through the digester tank. It checks flow pattern, mixing intensity, and dead-zone formation on screen first, catching stagnant pockets while they’re still cheap to fix, since correcting a poor mixing pattern after installation is far more expensive.
Flow pattern and tank turnover, dead zones near the base and corners, impeller tip speed and turbulence level, scum-breaking behavior at the surface, mounting stability and vibration control, and power draw ahead of final sizing.
It means better impeller selection for the actual tank volume and feedstock type, more consistent slurry circulation, a lower chance of poor gas yield, and more confidence moving from pilot trials to full plant operation. It also means the motor and shaft design gets optimized before anything is fabricated.
Digester mixing sounds straightforward until it has to work on a real tank, with real feedstock, under real process conditions – that’s the part Premix Technologies pays close attention to on every Central Mixer for Biogas Digesters it delivers. The process starts with a conversation about the tank and the feedstock, then moves through design, manufacturing, and support after installation. Operating out of Ahmedabad, the team has built enough of a track record that biogas plants looking for reliable Central Mixer for Biogas Digesters Suppliers and Central Mixer for Biogas Digesters Exporters tend to find their way to Premix Technologies.
Reach out to Premix Technologies for a proposal built around the actual tank volume and digestion chemistry, not a generic one lifted from a catalog. Domestic and international buyers work with Premix Technologies as their preferred Central Mixer for biogas digester exporters.
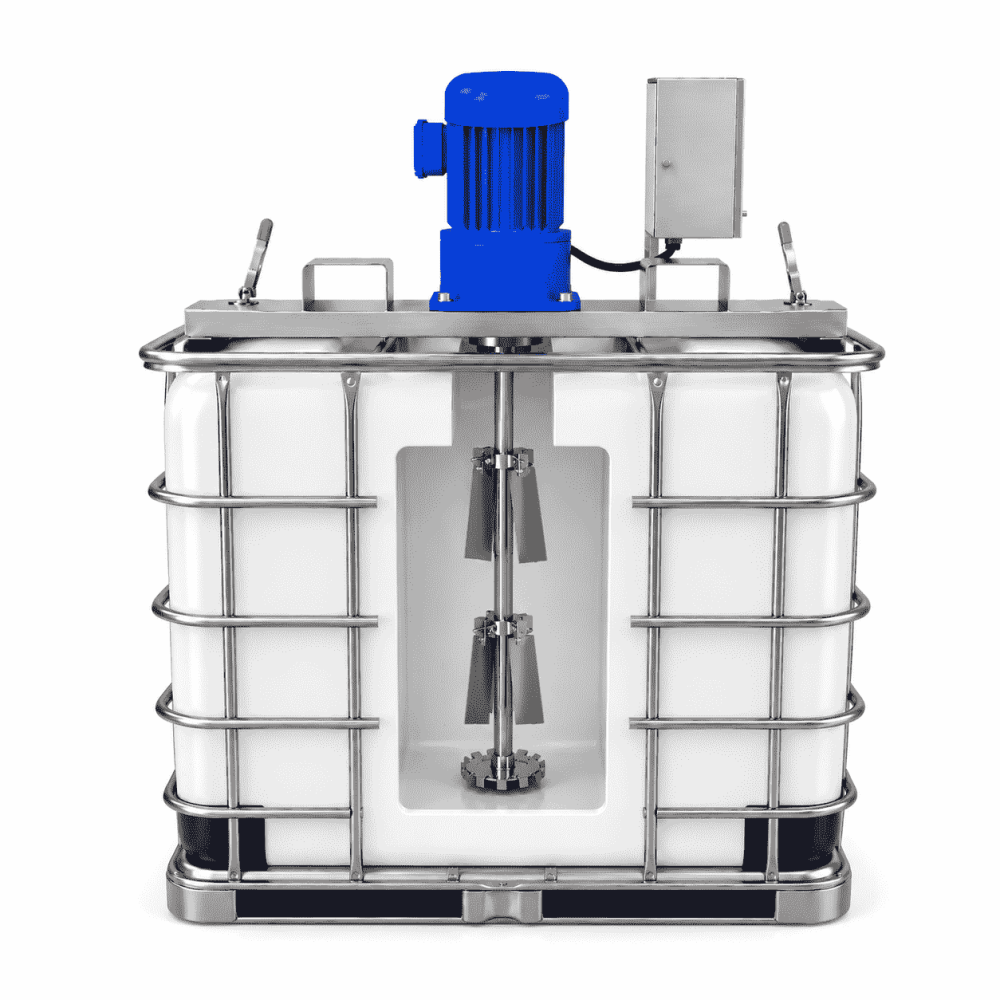
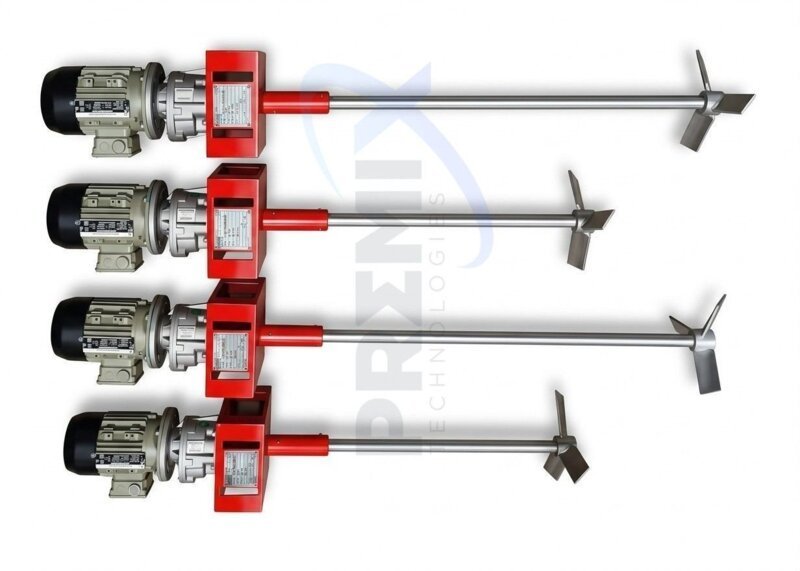
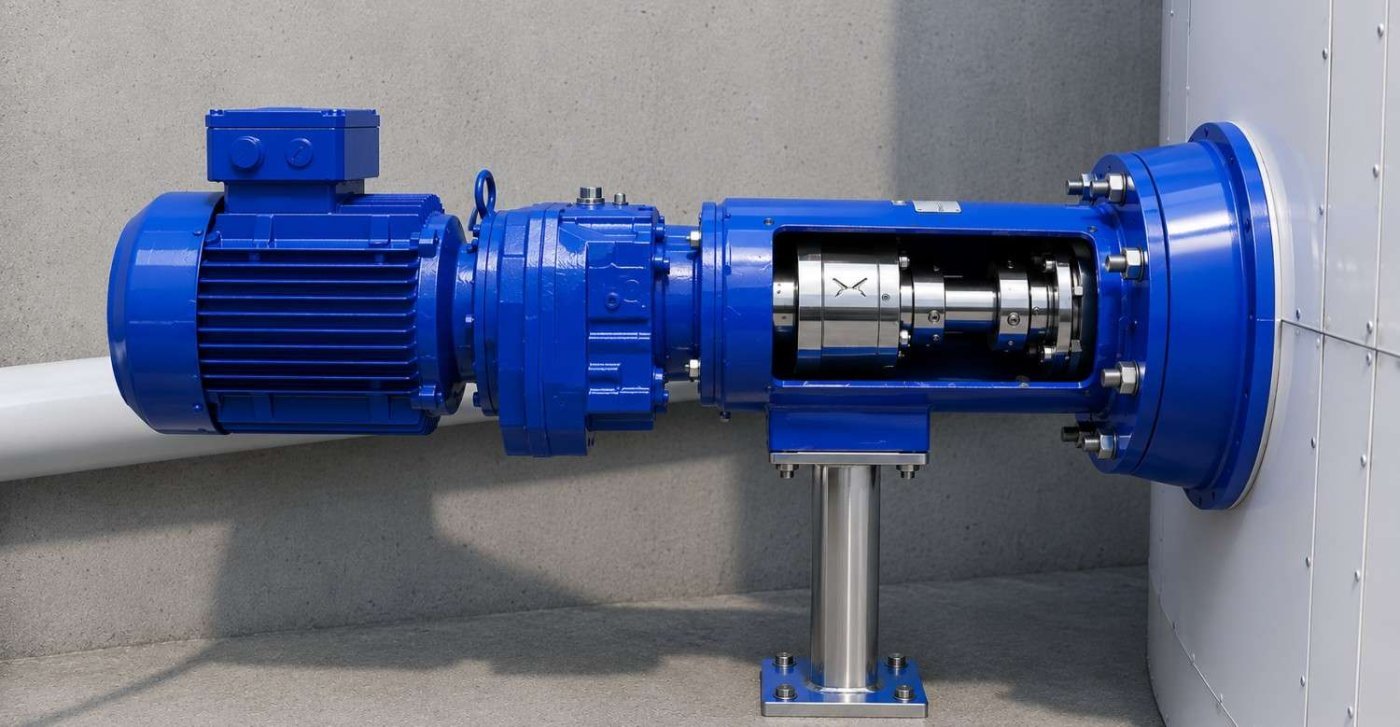
A Central Mixer for Biogas Digesters is used to keep feedstock, sludge, and bacteria evenly circulated inside an anaerobic digester tank. It prevents scum formation at the surface, stops solids from settling at the base, and ensures the microbial population stays in contact with fresh feedstock for consistent biogas yield.
Premix Technologies supplies Central Mixer for Biogas Digesters to municipal wastewater treatment plants, agricultural and farm-scale biogas plants, CBG (Compressed Biogas) facilities, distilleries, food processing units, and poultry & dairy waste digestion plants. As an experienced Central Mixer for Biogas Digesters manufacturer based in Ahmedabad, we’ve handled digester mixing requirements across all these sectors from a single manufacturing facility in Gujarat.
Share your tank volume, feedstock type (manure, sludge, food waste, spent wash, etc.), total solids percentage, and retention time. Our engineering team reviews these inputs and, where needed, runs a CFD study before recommending the right impeller type, shaft length, drive power, and wetted materials.
Yes. Premix Technologies supplies the complete Central Mixer for Biogas Digesters assembly, including the central shaft, impeller, gearbox, motor, mounting structure, and where required, explosion-proof (ATEX/IECEx) drive components – fully engineered and tested before dispatch.
Most manufacturers quote a Central Mixer for Biogas Digesters straight off a catalog. At Premix Technologies, engineering starts with the actual tank geometry and feedstock behavior – often backed by CFD flow studies – before any impeller or drive gets selected. That process saves biogas plant operators from poor gas yield, premature wear, and repeat purchases.
Have questions about our products or need a customized solution? Our team is ready to assist you with expert guidance, technical support, and reliable service. Reach out to us today and let’s build efficient solutions together.